How 2BV Vacuum Pumps Efficiently and Safely Handle Moisture and Condensable Vapor
2026-09-11 16:54:04
Read:
Share:
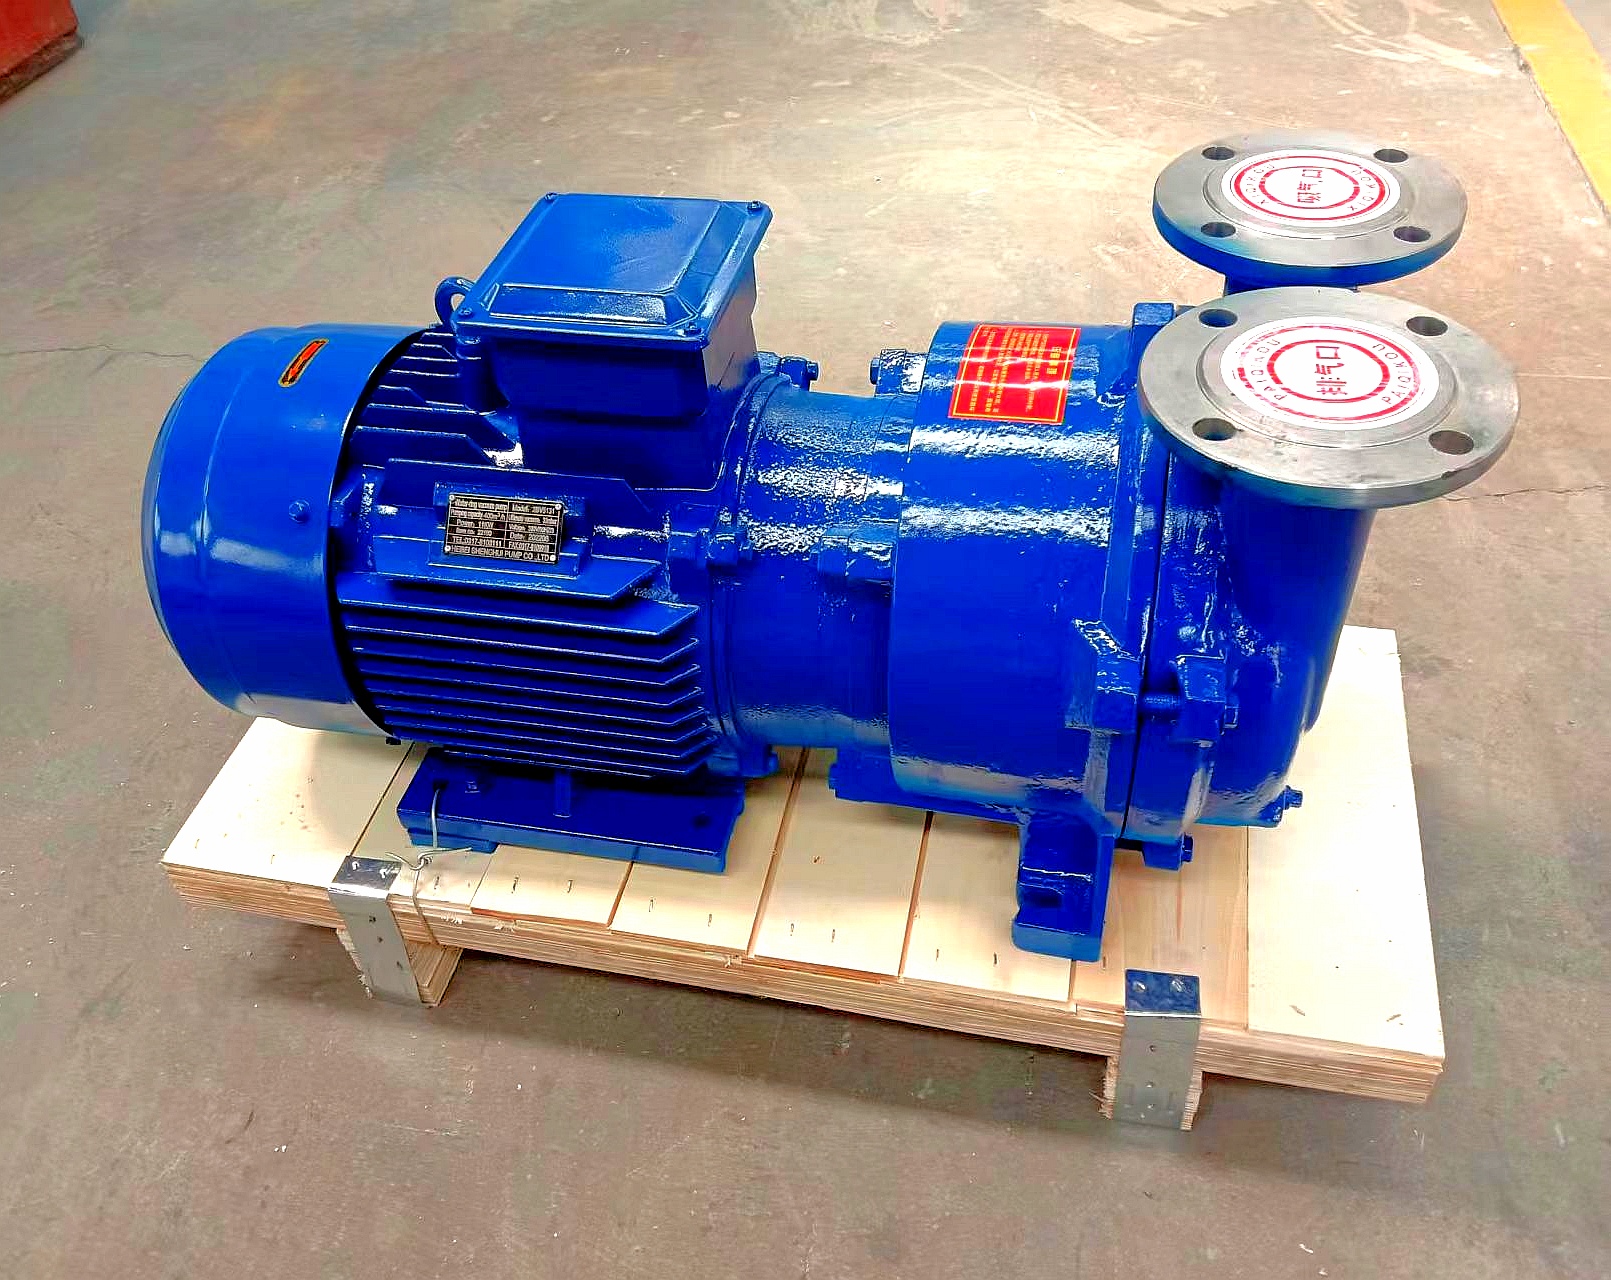
In processes involving vacuum drying, evaporation and concentration, and industrial degassing, the medium extracted by the vacuum system is not completely dry air, but rather a mixture of gases containing large amounts of moisture and vapor. If the equipment lacks sufficient capacity to handle vapor condensation, it is prone to problems such as a drop in vacuum level, unstable operation, and an increased likelihood of equipment failure and downtime. The 2BV vacuum pump, however, utilizes a liquid ring operating principle to deliver stable and efficient performance when handling moist air, wet steam, and media containing small amounts of liquid, while significantly reducing safety hazards caused by fluctuations in operating conditions.
This equipment treats the medium utilizing a near-isothermal compression process, making it ideal for long-term operation in environments involving moist gases and wet steam. Upon startup, the working fluid in the pump chamber forms a stable liquid ring, directing the drawn-in liquid into a chamber located between the impeller and the liquid ring. The continuous rotation of the impeller gradually reduces the volume of the gas and compresses it, facilitating the intake, compression, and discharge of the gas. During this compression process, the gas maintains full contact with the liquid, allowing the heat generated by compression to be rapidly absorbed by the liquid and ultimately achieving an isothermal compression process. This process mitigates, to a certain extent, the heat generated by rapid temperature increases, thereby ensuring safe and stable operation when pumping flammable and explosive gases.
For condensable vapor, the vapor condenses after entering the vacuum pump, transforming into a liquid as pressure and temperature change; eventually, the condensate enters the pump’s working fluid system. This equipment uses the working fluid to form a liquid ring and compress the gas, allowing the condensate to participate in the pump’s internal circulation alongside the working fluid, thereby reducing, to a certain extent, the impact of vapor condensation on the pump’s normal operation. In contrast to vacuum pumps that cannot operate under wet conditions, when moisture enters the 2BV series, the operating characteristics of its liquid ring ensure that a small amount of liquid entrainment is well compatible with its operating principle. Hence, in systems where the air contains high humidity, water vapor, or condensate, the 2BV vacuum pump remains capable of maintaining a stable pumping process throughout operation. This design also minimizes direct contact between mechanical components during gas compression, significantly decreasing the risk of mechanical wear caused by moisture-laden media entering the pump housing.
To meet the demands of long-term operation under low suction pressure conditions, this equipment can be configured with a cavitation protection system. When the suction pressure approaches the lower operating range, this system mitigates the adverse effects of cavitation on pump operation. For equipment that requires continuous extraction of moist vapor while maintaining a high vacuum level, this design effectively enhances stability during low-pressure operation. Furthermore, the equipment’s monoblock design reduces the installation space required by traditional coupling arrangements, while also facilitating installation and maintenance.
The 2BV liquid-ring vacuum pump is well-suited for industrial vacuum systems that handle water vapor, humid air, and liquids. It provides stable pumping capacity for vacuum drying, evaporation, degassing, filtration, vacuum packaging, and other industrial vacuum processes.